Cleaning an industrial chiller is an action that is easily postponed until production forces a shutdown. Still, in most situations, maintenance of the chiller can be accomplished without interrupting production, as the measures are planned in advance and implemented systematically. In this guide, we will go through how to properly clean a chiller alongside an ongoing process, what tools you need, and how to ensure that the unit operates flawlessly after the cleaning.
In environments handling bulk materials, chillers are constantly exposed to wear materials, dust, and high temperatures. This accelerates the accumulation of coatings and material residues on the internal surfaces and cooling elements of the equipment. Uncleaned chillers gradually lose their cooling capacity, which is reflected in increased output temperatures and increasing energy consumption. Discover our cooling solutions and see what options are available for demanding destinations.
Necessary tools and safety preparations before cleaning
Start by mapping out what kind of material the cooler handles. Hot metallurgical slags, ashes, and fine dust require different levels of protection than more humid by-products. Safety preparations are not just formalities; they determine how the cleaning process can be carried out while the process is underway.
Gather the following tools and protective equipment before you begin:
- Personal protective equipment: respiratory protection (at least P3 class in a dusty environment), heat-resistant gloves, protective goggles and, if necessary, a heat-resistant protective suit
- Pneumatic blower or industrial vacuum cleaner for removing material residues
- Brushes and brush heads for mechanical cleaning of coated surfaces
- Thermometer or thermal camera for checking the temperature of surfaces before touching them
- Locking devices (LOTO locks) for ensuring serviceable maintenance locks and inspection openings
- Dust collector or closed container for cleaning material that is being removed
Before starting the cleaning, make a written risk assessment together with the process controller. Determine which parts of the equipment can be opened during an ongoing process and which require local isolation. In many chiller solutions, the service doors and inspection openings are designed so that they can be safely opened without shutting down the entire unit, but this must always be verified from the equipment documentation and the manufacturer’s instructions.
Performing cleaning alongside an ongoing process
Cleaning alongside an ongoing process is based on the fact that you operate the equipment in different zones in an orderly manner without interrupting the material flow. This requires good cooperation with the process operator to prepare for variations in the material flow during cleaning.
Proceed with the cleaning in the following order:
- Open the first inspection hatch from the device's input end. Check the temperature before inserting a hand or tool inside.
- Remove loose material using a compressed air blower or an industrial vacuum cleaner. Direct the air flow so that the loose dust is directed into the collection container and does not spread into the environment.
- Clean the coated surfaces mechanically brushed or scraped. Pay special attention to the gaps between the cooling elements, where the material accumulates more easily.
- Close the hatch and move to the next zone. Allow the previous zone to settle down before you open the next hatch.
- Repeat the action to the device's removal port.
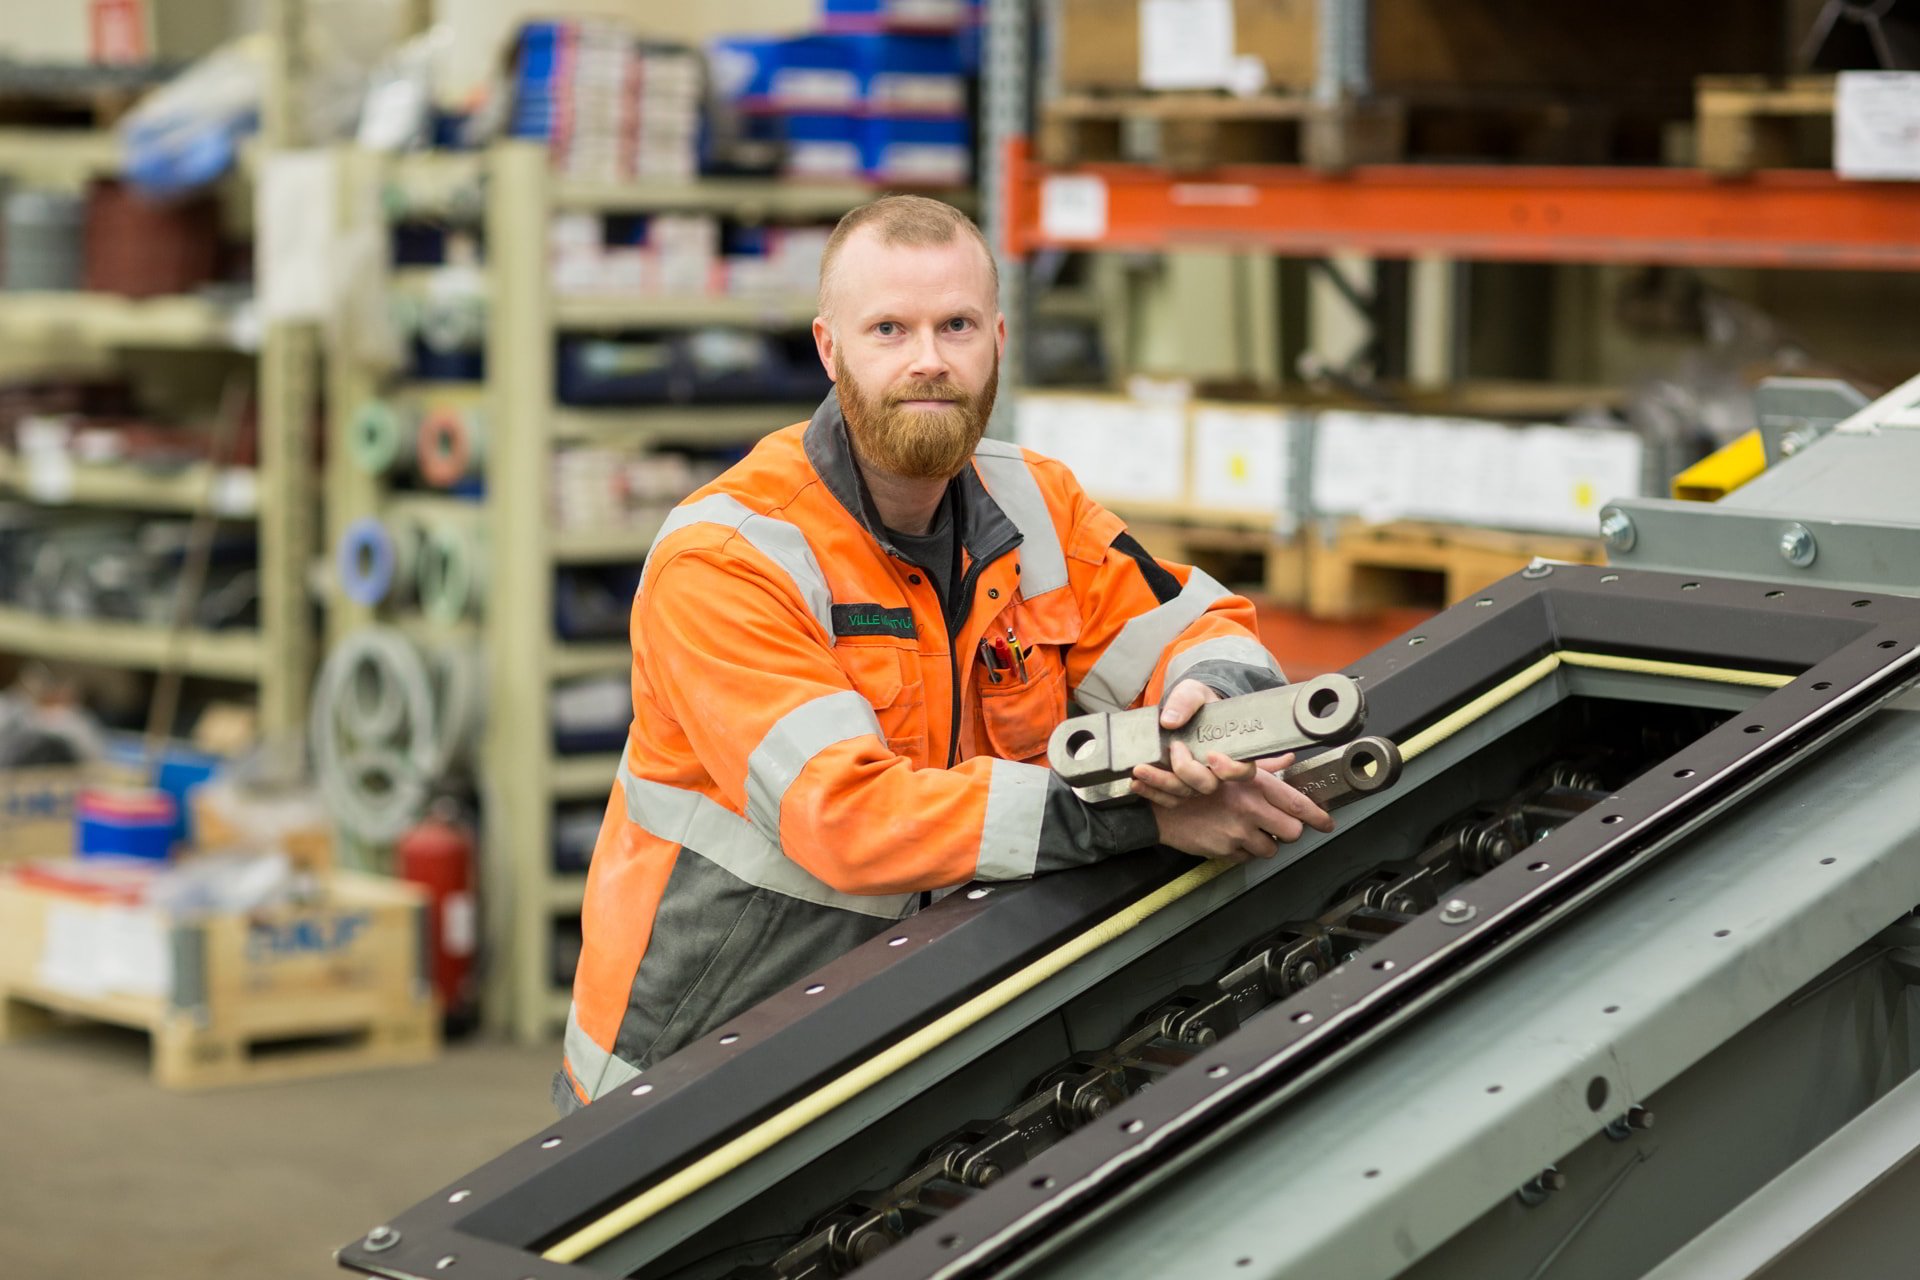
If the chiller has removable panels, such as in modular rotary chillers, you can remove an individual panel for cleaning or inspection without interrupting the operation of the unit entirely. This is a significant advantage compared to traditional solutions where the entire unit has to be opened for maintenance. Contact us, If you want to find out whether your hardware is suitable for this method of operation.
Checking the cleaning result and ensuring operational capability
Once cleaning has been completed in all zones, it is time to ensure that the device operates as intended. A mere visual inspection is not enough; operational condition must be verified using measurable values.
After cleaning, check the following:
- Measure the output temperature of the material and compare it to the process target value. If the temperature has dropped towards the target value, the cleaning has been successful.
- Check all the hatches and panels Visually. Make sure the seals are intact and the fasteners are in good condition.
- Track your device's energy consumption for the next hour of use. A cleaned cooler consumes less energy compared to a broken one, with the same cooling power.
- Record the cleaning day, any detected damage, and the amount of material residues in the maintenance logbook. This information is valuable in determining the next cleaning interval.
If the outlet temperature does not drop as expected after cleaning, the cause may be mechanical damage to the cooling elements or the cooling water circuit. In this case, a deeper inspection is required, which may require a short production stoppage. However, early detection is always better than waiting until the device stops functioning completely. See our references and see how similar situations have been resolved in different process environments.
Optimizing cleaning intervals according to material properties
One of the most common mistakes in servicing industrial cooling systems is that the cleaning interval is determined based on the material’s behavior rather than the calendar. Six months is suitable for one material, but for another material the same device can fail within a few weeks.
When optimizing cleaning intervals, the following factors should be taken into account:
- Material moisture content: Wet materials, such as sawdust and manure, adhere more strongly to surfaces than dry materials and significantly shorten the cleaning interval.
- Particle size and distribution: Fine-grained materials, such as fly ash or battery dust, penetrate into small gaps and require more thorough cleaning than coarser materials.
- Material sintering tendency: Some materials, such as certain slags and limestone dust, harden under the influence of heat and form hard-to-remove layers. In these cases, more thorough cleaning is clearly more cost-effective than the mechanical removal of hardened layers.
- Load level of the process: A device that runs at full capacity continuously will get dirty more quickly than one that operates with partial load.
Build a cleaning schedule by systematically monitoring the output temperature. When the temperature starts to rise without changing the process conditions, it is a sign that cleaning is necessary. By recording the time of this rise over several periods, you can obtain a reliable picture of what the cleaning interval corresponds to exactly for your process needs.
Kopar designs cooling solutions based on the actual properties of the material, and if necessary, the behavior of new materials can be tested in a test facility before final sizing. This reduces the risks associated with commissioning and helps determine the correct maintenance interval in advance. Discover our cooling solutions or Get in touch, So let’s go through how the solution fits your specific process.
You have a challenge that needs solving?
Let us help! Contact us for more information about our products and services.